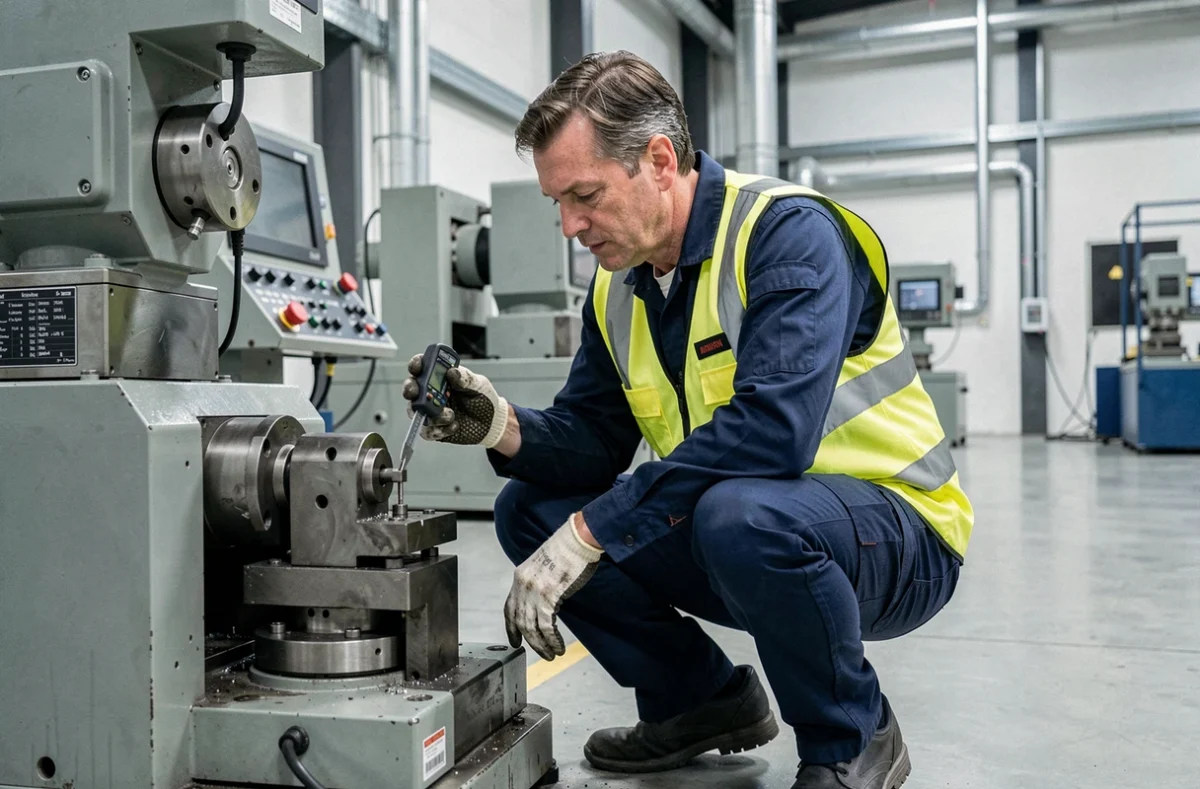
Unplanned downtime costs more than spare parts. In 2026, industrial maintenance finds itself at the intersection of three simultaneous pressures: production rates that can no longer tolerate any interruption, an expanding European regulatory framework that now includes software and connected layers, and field teams whose skills must evolve at the same pace as digital tools. This context reshapes how manufacturers manage the reliability of their equipment.
OT Cybersecurity and Maintenance: The Regulatory Link That Traditional Plans Overlook
Most industrial maintenance guides address digitalization from the perspective of IoT sensors or CMMS. They overlook a constraint that has become structural: the security of operational technology (OT) is now an integral part of production continuity.
The NIS2 directive requires affected industrial sites to conduct an asset inventory, implement strict segmentation between IT and OT networks, and establish formal patch management. In practical terms, every firmware update of a connected controller falls under maintenance, just like a bearing replacement.
The Cyber Resilience Act, with notification obligations to ENISA that came into effect on September 11, 2026, extends this logic to manufacturers of products containing digital elements. IoT sensors, supervisory software, programmable controllers: every connected component used in the maintenance chain must be subject to vulnerability tracking. A maintenance manager following industrial news on Airbuzz understands how these requirements change the daily scope of interventions.
The concrete risk: a cyberattack on a supervisory system can cause a production halt as abrupt as a mechanical failure. The difference is that recovery after a cyber incident often takes several days, compared to a few hours for a part replacement.
Predictive Maintenance in Production: Organizational Limits Before Technology
Deploying predictive maintenance algorithms on industrial equipment seems appealing. Field feedback varies on this point. Several sector analyses show that the main obstacle is not technological but organizational.
Data Quality and Machine Connectivity
Before training an AI model, reliable data is needed. On a heterogeneous fleet (old machines without native sensors, different communication protocols), data collection is fragmented. Machine connectivity determines the viability of any predictive project.
Some industrial sites invest in additional IoT sensors without verifying that their network can support the volume of data generated. The result: inconsistent alerts, false positives that erode technicians’ trust, and a gradual return to manual rounds.
Field Skills and Adoption
A maintenance technician trained in traditional preventive methods does not become a data analyst in a few weeks. Field feedback indicates that successful predictive projects share a common trait: they involved the teams from the scoping phase, not just during deployment.
- Check the connectivity and compatibility of machine protocols before purchasing sensors
- Audit the quality of historical data available in the existing CMMS
- Train technicians to interpret predictive alerts, not just to receive them
- Define a minimum confidence threshold before triggering an automated intervention
Without these prerequisites, predictive maintenance remains an investment without measurable return.
Spare Parts Management and Downtime Costs: Arbitrating Without Over-Stocking
Spare parts management concentrates a constant tension between two risks: over-stocking (tied-up capital, obsolescence) or under-stocking (prolonged production halt waiting for a critical part).
Recent CMMS tools allow for cross-referencing intervention histories with supplier lead times. The goal is to calculate a safety stock for critical references, based on the actual frequency of failures rather than a flat estimate.
However, available data does not always allow for distinguishing failures due to normal wear from those caused by upstream process defects. A reliable root cause diagnosis reduces costs more than a replenishment algorithm.
Prioritizing Equipment by Production Criticality
Not all equipment deserves the same level of maintenance. A compressor feeding a unique assembly line does not carry the same weight as a redundant conveyor. Classifying by criticality allows for focusing preventive interventions and spare parts stock on machines whose downtime truly halts production.
- Class A: immediate production halt, no redundancy, critical parts stock mandatory
- Class B: gradual degradation, temporary workaround possible
- Class C: limited impact, corrective maintenance acceptable
This prioritization avoids dispersing maintenance budgets on low-impact interventions while protecting positions where a failure costs the most.
Digitalization of Maintenance: What CMMS Alone Does Not Solve
Installing a CMMS does not transform an organization. The tool structures work orders, centralizes histories, and facilitates the planning of preventive interventions. What it does not do: solve communication issues between production and maintenance, nor compensate for a lack of reliability in field data entry.
Digitalization works when technicians actually enter data after each intervention. If data entry is perceived as an administrative burden without visible return, the foundations degrade within months. Maintenance managers who achieve sustainable adoption share performance indicators derived from the CMMS with the teams: availability rates, mean repair times, cost evolution per equipment.
The reliability of industrial equipment in 2026 depends less on technological sophistication than on the rigor with which fundamentals are applied. A clear criticality classification, accurately captured field data, regulatory monitoring of cyber obligations: these three pillars determine whether maintenance remains a cost center or becomes a lever for production performance.